How to Make a Damascus Knife at Home
Many people assume crafting patterned Damascus steel requires an industrial factory or lost ancient secrets. That belief is common, but modern knifemakers make this metal by stacking alternating sheets of steel and forge-welding them into one solid bar. Forge welding means heating the steels until they glow bright yellow and hammering them so they fuse together. Shaping the welded block creates the pattern, and a quick acid dip makes the swirling lines visible.
How you tackle this project depends on your workshop setup. Heating and bonding raw metal by hand demands a forge, an anvil, and high heat so the layers do not peel apart. Choosing compatible steels with clear color contrast gives you distinct light and dark bands. Beginners without heavy hammering tools can also buy pre-layered Damascus steel bars and shape them directly. Here is how each method works so you can pick the right path.
What Modern Damascus Steel Actually Is
Modern Damascus steel, known among knifemakers as pattern-welded steel, combines two or more types of steel into a single layered piece. You take alternating sheets of metal, heat them in a forge until they glow bright yellow, and hammer them until they fuse into one solid bar. The wavy lines do not come from paint, acid stencils, or surface tricks. They are the actual seams between different steels running through the core of the blade.
Knifemakers commonly stack 1095 high-carbon steel with 15N20 alloy steel. High-carbon steel is a harder metal that stays sharp longer but requires dry wiping and light oiling to prevent rust spots. In contrast, 15N20 contains about two percent nickel, which resists acid. When you dip the finished blade in acid, the 1095 turns dark gray while the 15N20 stays bright silver. This contrast creates the bold lines seen on authentic Japanese Damascus steel chef knives. You are simply bonding two predictable steels together under controlled forge heat.
Ancient legends often confuse pattern welding with historic crucible steel called Wootz, but modern knifemakers rely on metallurgical science rather than lost myths. Today, you are deliberately bonding predictable alloys together under clean, tightly controlled heat. The resulting knife balances edge retention with visual depth.
Materials and Tools You Need in Your Shop
Forging layered steel demands more heat and force than shaping a simple single-steel blade. Gathering the right setup beforehand keeps you safe and prevents cracked seams.
- Complementary steel bars: Clean plates of 1095 and 15N20 cut to identical lengths and widths. Matching sizes ensures uniform heat throughout the stack.
- High-heat forge: A propane or coal forge reaching 2,300 degrees Fahrenheit. Standard propane plumbing torches cannot reach welding heat.
- Anvil and hand hammer: A flat anvil face and a balanced 2.5-pound to 3-pound hammer to move steel quickly before it cools.
- Welding flux: Anhydrous borax powder used to block air and dissolve crusty scale from glowing steel.
- Welder or steel wire: A basic welder to tack the stack corners and attach a long steel holding rod. Heavy steel wire wrapped tightly works if you lack a welder.
- Belt grinder: A 1x30-inch or 2x72-inch electric sander with coarse ceramic and fine finishing belts.
- Protective safety gear: Eye protection, face shield, earplugs, leather apron, and non-synthetic cotton clothing that will not melt against sparks.
Step-by-Step Guide to Stacking and Forge-Welding the Billet
A billet is a stack of steel bars prepared for forging. Forge welding means joining glowing metals by hammering them until their crystal grains lock together. Delamination, or layers peeling apart, happens when dirt, air, or cold temperatures get trapped between the bars. Follow these exact steps to ensure a solid bond:
- Grind every steel plate down to bare, shiny metal.
Reason: Surface rust and mill scale block direct contact between the metals, causing internal voids that split open later.
- Stack the bars in alternating layers of 1095 and 15N20.
Reason: Alternating the alloys guarantees crisp visual contrast between dark high-carbon steel and bright nickel steel across every layer.
- Tack-weld the corners and weld a long rebar handle to one end.
Reason: Corner tacks stop the plates from sliding out under hammer blows, while the handle keeps your hands clear of forge flames.
- Heat the stack to a dull red glow and sprinkle anhydrous borax flux over all seams.
Reason: The melting borax forms a liquid glass seal that keeps oxygen out and dissolves crusty oxides.
- Soak the billet until it reaches a bright yellow heat.
Reason: The steel must hit roughly 2,300 degrees Fahrenheit so the iron crystals can fuse across the boundaries.
- Set the weld using overlapping, rapid, medium hammer strikes from the center outward.
Reason: Working from the center squeezes out excess liquid flux and bonds the glowing faces without shearing the seams.
- Return the billet to the forge the moment the bright yellow color begins to fade.
Reason: Hammering steel below welding heat causes delamination, tearing the uncured seams apart.
- Reheat to welding temperature and draw the block into a longer bar.
Reason: Once fully fused, heavy hammer strikes can safely stretch the thick block into usable knife stock.
Patterning, Shaping, and Heat Treating the Blade
Once the billet is solid, you can multiply layers or twist the bar to develop patterns. Cutting the bar into four pieces, grinding the surfaces clean, and re-welding them turns a 7-layer billet into 28 layers. Doing it again produces 112 layers. Twisting the glowing bar creates spiral star effects, while drilling shallow divots before forging creates a raindrop pattern.
Turn your patterned bar into a knife through these shaping and heat-treating stages:
- Taper the tip and forge the tang. Choose between a full tang, meaning one solid piece of blade steel extending all the way through the handle, or a partial tang, where the blade metal narrows or stops inside the handle. A full tang offers maximum strength for heavy cutting.
- Grind the blade bevels. Use a coarse belt on your sander to shape the primary bevels. Keep the cutting edge about one millimeter thick so the thin steel does not warp during the quench.
- Normalize the blade three times. Heat the shaped steel to a dull red glow and let it cool completely in still air. This relieves internal stresses and shrinks the steel grain.
- Quench in warm knife oil. Heat fast-quenching oil to about 130 degrees Fahrenheit. Heat the blade until a magnet no longer sticks to it, then lower it straight down into the oil.
- Temper in a home oven. Hardened steel straight from the quench is brittle. Bake the blade at 400 degrees Fahrenheit for two separate two-hour cycles to give the steel toughness.
Acid Etching to Reveal the Damascus Pattern
When the blade leaves the tempering oven, the metal looks like plain gray steel. The Damascus pattern appears only after fine sanding and a controlled acid etch.
Hand-sand the blade through progressive grits up to 800 or 1,000 grit using a solid sanding block. Degrease the steel thoroughly with acetone or rubbing alcohol. Any leftover finger oil blocks the acid and leaves blotchy marks.
Submerge the clean blade in an acid bath of ferric chloride mixed with three parts distilled water. Let it soak for five to ten minutes. The acid eats into the 1095 high-carbon steel, turning it dark charcoal gray. The nickel in the 15N20 resists the chemical and stays mirror-bright.
Pull the blade out, rinse it with clean water, and dunk it in a baking soda bath to neutralize remaining acid. For a darker contrast, soak the etched steel in warm instant coffee for two hours. Wipe it dry and coat it with mineral oil to prevent immediate surface rust.
The Stock Removal Shortcut: Using Pre-Welded Steel
If you want to build a Damascus knife but do not own a forge, anvil, or welder, starting with a factory-welded Damascus steel billet is an excellent shortcut.
Using stock removal, you shape the blade entirely through grinding:
- Trace your profile directly onto the steel bar and cut out the profile using an angle grinder or bandsaw.
- Grind the primary bevels on a 1x30 or 2x72-inch belt sander, checking your bevel symmetry against a scribed centerline.
- Send the shaped blade to a commercial heat-treating service to ensure exact hardness without shop equipment.
- Hand-sand the tempered blade and etch it in ferric chloride to reveal the pattern.
Stock removal eliminates the fear of delamination, letting you practice handle construction and edge geometry. You can master grinding a steep 15-degree slicing edge per side for delicate Japanese kitchen knives or a sturdy 20-degree utility edge for pocket and hunting knives. If you want to study how factory blades balance layered outer steel with high-performance cores, exploring high-carbon steel knives provides a helpful benchmark.
How Knifemaking Reference Guides Help You Succeed
Forging layered steel involves strict temperature windows, alloy pairing, and crucial shop safety precautions. Ruining hours of work on an expensive billet because of a cold strike or incorrect soak time is a common beginner frustration.
Knifemaking guidebooks and visual reference manuals give you proven workshop roadmaps. When selecting a reference manual for your bench, look for:
- Visual temperature charts: Color photography illustrating exact steel colors, from dull cherry to bright yellow welding heat.
- Alloy matching guides: Reference data listing which steels weld smoothly together and share compatible quench rates.
- Pattern layouts: Step-by-step schematics showing how ladder cuts, twist rates, and surface grinds produce specific blade visuals.
- Workshop safety guides: Clear instructions for managing toxic flux vapor, fine grinding dust, and hot oil quench flare-ups.
Keeping a dependable reference manual beside your anvil eliminates guesswork during fast-moving forge heats.

- TAR Score9.6
TAR Score is a ranking system developed by TopAppliancesReviews.com. TAR score has no relationship or impact from any manufacturers or sales agent websites. Learn more
- BrandSchiffer Craft

- TAR Score9.2
TAR Score is a ranking system developed by TopAppliancesReviews.com. TAR score has no relationship or impact from any manufacturers or sales agent websites. Learn more
- BrandSCHIFFER PUBLISHING LTD
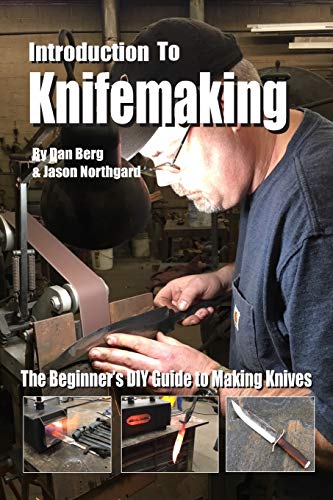
- TAR Score9.2
TAR Score is a ranking system developed by TopAppliancesReviews.com. TAR score has no relationship or impact from any manufacturers or sales agent websites. Learn more
- BrandIndependently Published

- TAR Score9.0
TAR Score is a ranking system developed by TopAppliancesReviews.com. TAR score has no relationship or impact from any manufacturers or sales agent websites. Learn more
- BrandLAP Lambert Academic Publishing
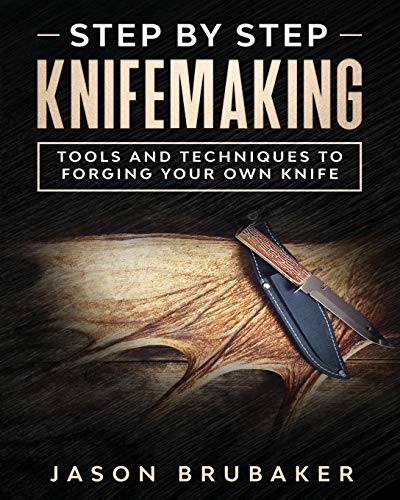
- TAR Score8.8
TAR Score is a ranking system developed by TopAppliancesReviews.com. TAR score has no relationship or impact from any manufacturers or sales agent websites. Learn more
- BrandIndependently Published

- TAR Score8.6
TAR Score is a ranking system developed by TopAppliancesReviews.com. TAR score has no relationship or impact from any manufacturers or sales agent websites. Learn more
- BrandN/A

- TAR Score8.0
TAR Score is a ranking system developed by TopAppliancesReviews.com. TAR score has no relationship or impact from any manufacturers or sales agent websites. Learn more
- BrandMajosta

- TAR Score7.8
TAR Score is a ranking system developed by TopAppliancesReviews.com. TAR score has no relationship or impact from any manufacturers or sales agent websites. Learn more
- BrandN/A
Last update on 2026-10-02 / Affiliate links / Images, Product Titles, and Product Highlights from Amazon Product Advertising API
Frequently Asked Questions
Can you forge Damascus steel without a power hammer or hydraulic press?
Yes, you can forge Damascus by hand using a standard blacksmith hammer and anvil. Keep your initial billet small, around seven to twelve layers and under one inch thick, so your arm can forge it quickly while it stays hot. Large billets lose heat too fast for manual hand hammering.
Why do the layers of a Damascus billet peel apart during forging?
Layers peel apart, or delaminate, when steel drops below welding temperature before the joints fully fuse. Trapped forge scale, inadequate borax flux, or dirty raw metal will also stop the layers from welding. If a seam begins splitting, stop hammering, reheat the steel, add flux, and tap it gently at yellow heat.
What is the safest way to dispose of spent ferric chloride acid?
Never pour ferric chloride down household drains because it rapidly corrodes copper, brass, and iron pipes. Neutralize the acid outdoors by slowly adding baking soda until all bubbling stops completely. Once neutralized, check with your local municipal waste facility for guidelines on disposing of heavy metal liquids.
How do you protect a finished Damascus knife from rusting?
Because carbon-steel Damascus contains no chromium, it is not rust-resistant stainless steel. Wash the blade by hand with mild soap right after use, dry it immediately with a towel, and never place it in a dishwasher. Wipe the blade down with a drop of food-safe mineral oil before putting it away.
Top Rated Best Quality Range Hoods: 2026 Expert Picks
The 12 Best Small Solar Generators 2026

10 Best Quality Semi Automatic Washing Machine of 2026 For Leak-Free Laundry

11 Best Small Washer Machine of 2026 For Everyday Laundry

12 Best Vibration Pads For Washing Machine of 2026 To Stop Walking and Shaking
11 Best Selling Front Load Washing Machine of 2026 For Quiet Odor-Free Laundry

11 Best Washing Machine For King Size Bedding of 2026 To Prevent Cycle Errors

10 Best Small Front Loader Washing Machine of 2026 For Tight Closets